Analysis and improvement of drop cable fiber attenuation problem
author: Zhejiang Linquick Technology Co., Ltd.
2023-09-01
First. Introduction
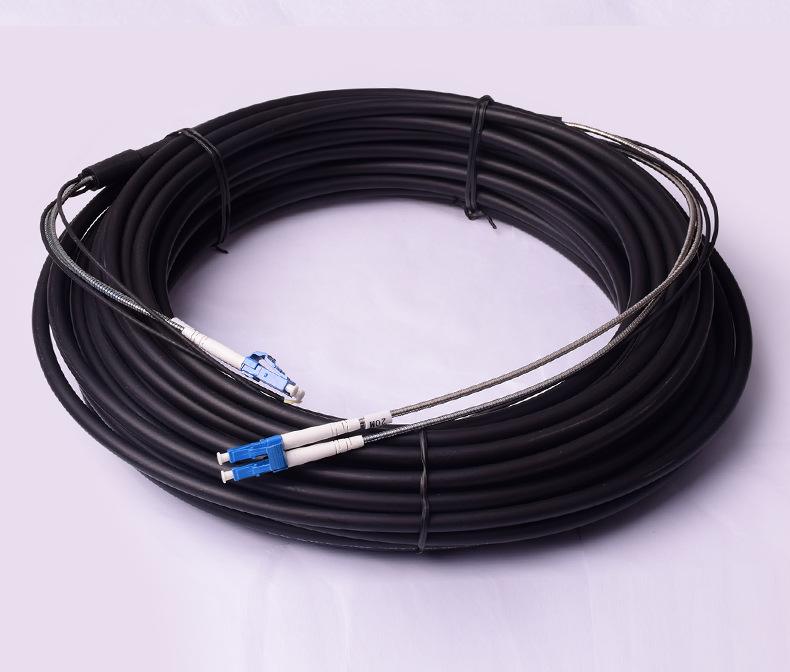
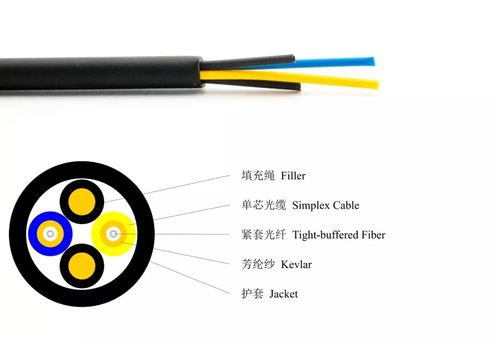
At present, broadband services represented by high-speed Internet services, image file processing, online music, animation downloads, online games, online education, etc., are developing rapidly, and bandwidth has become a bottleneck restricting Internet performance, while FTTH with high bandwidth has become the best guarantee to realize the "three networks in one" of telephone, cable TV and Internet access. Drop cable (also known as leather cable) as a large-scale application to the FTTH network user introduction section of the optical cable, has a broad market prospects, in the premise of meeting the needs of users, to ensure the quality of the product, and butterfly cable production after the detection of fiber attenuation (hereinafter referred to as attenuation) high problem.
This paper mainly analyzes the cause of this problem, carries on the process control, puts forward the corresponding improvement measures, reduces the occurrence of this problem, improves the product quality.
Second. Standard requirements
Dop cable attenuation refer to YD/T 1997.1-2014.
Dop cable attenuation refer to YD/T 1997.1-2014.
Third. Reason analysis
According to the statistical data of quality problems and the feedback of the on-site inspection of the process personnel, the reasons for the high attenuation of the butterfly cable are analyzed from five aspects: man, material, machine, method and ring.
1. People (human factor)
① The operator is not installed in place when installing the optical fiber disc and strengthening parts, and there is jitter in production, resulting in sudden fluctuation of tension;
The mold selection and installation are not in place, the mold is not checked, and the mold defect scratches the optical fiber;
③ The extrusion temperature and water temperature of the sink are not fully checked before getting on the car;
④ Other operations that do not meet the requirements of the process card.
2. Materials (material factors)
(1) The optical fiber itself is defective, injured in the coloring process or its parameters do not meet the standard;
(2) Sheath material is not properly stored moisture or material contains large impurities, impurities or moisture compression to the optical fiber during extrusion;
(3) The reinforcement has the phenomenon of rust, which is scraped off on the mold to form impurities, and the optical fiber is compressed by rust during extrusion;
④ The barrel core of the disc is not smooth and flat, there is a large height difference, and the butterfly cable is stressed when the disc is installed.
3. Machine (equipment factor)
① The mold in the head is worn during production and scratches the optical fiber;
(2) The guide wheel bearing or tension wheel on the optical fiber routing path is damaged, resulting in hard tension on the optical fiber, resulting in defects;
③ The temperature in each area of the extruder is out of control, producing coke and pressing the optical fiber;
④ The fiber dehumidification heating and drying device is not opened or the power is not up to standard, and it does not play the role of dehumidification and preheating.
4. Method (process factor)
(1) In the previous coloring process, the optical fiber is not cured well, resulting in residual colorant on the guide wheel and die on the wire path. After long-term accumulation, the residual colorant becomes hard, which is easy to scratch the optical fiber, or adhere to the optical fiber into the cable, and the residue compresses the optical fiber in a tiny space;
(2) The pay-off tension of the optical fiber, the pay-off tension of the reinforcing part, and the take-up tension are too large or too small;
③ The technician does not check every day according to the process inspection requirements, resulting in production personnel only to catch up with the progress, and reduce or ignore the process requirements.
5. Environment (environmental factors)
① The production workshop of butterfly cable is generally open, and there are more dust or impurities visible to the naked eye, which are attached to the optical fiber routing path and the sheath material will be brought into the mold, and extrusion with the material is easy to press the optical fiber or cause material disconnection.
(2) The temperature and humidity of the workshop environment is not controllable, especially in the Meiyu season, the workshop humidity is large, the temperature difference is obvious, and the optical fiber is seriously damp; The wet optical fiber extruded sheath, after about 150℃ head extruded sheath, moisture in the mold instant gasification, gasification state of water vapor can not be excluded through the sheath, remain in the butterfly cable, small space to produce pressure on the optical fiber.
Fourth. Process control and improvement measures
1. Production personnel play a dominant role in the production link, and self-test is needed in the upper and lower production lines to check whether the optical fiber and reinforcement parts are mispositioned and cause tension instability. Operate strictly according to the process card, regularly check the optical fiber pay-off tension, wire tension and take-up tension, and regularly check and record.
2. Use graded cooling method for cooling, 4 meters hot water tank and 12 meters cold water tank cooling, hot water and cold water are controlled at 50±2℃ and 30±2℃ respectively.
3. The technician shall strengthen the process inspection of the coloring process, check the cleanliness and quality of the mold, nitrogen flow rate, cleanliness and quality of the quartz tube and mirror, as well as the coloring ink, so as to prevent the poor curing and decolorization of the coloring fiber, which can effectively avoid the decolorization and plugging of the mold hole after flowing into the production process of the butterfly cable sheath, resulting in the fiber rubbing force, resulting in loss. Production personnel and technical personnel regularly check and clean the device on the guide wheel and the optical fiber wire diameter, and clean the dirt and residual coloring agent with alcohol.
4. The mold needs regular inspection, and the shape size of the cable also needs regular inspection, especially the first and last one of each shift, which can reflect the wear state of the mold, and timely replacement of the mold that does not meet the requirements.
5. The sheathing material should be kept properly to prevent moisture from the material. During processing, it should be preheated and dried at 60℃. The mouth of the bag should not be opened too large to reduce the entry of impurities such as dust, and the unused sheath material should be sealed as far as possible.
6 steel wire reinforcement should be purchased as needed, should not be stored for a long time, if the environment is wet, it will lead to rust.
7. When the attenuation required by customers is relatively strict, the optical fiber should be produced after index screening.
8. Dry and preheat the optical fibers, and install an infrared light on the pay-off rack.
9. Install a wire diameter heating device as shown in Figure 2 in the path of the optical fiber, dehumidify and preheat the optical fiber and reinforcement, and regularly test its power and effect. The production speed is 100m/min, and the preheating temperature is 90±2℃.
10. The equipment department should strengthen inspection, regularly check extrusion temperature, etc., and formulate and implement regular equipment maintenance system.
 Analysis of advantages of Copper cables and Optic fiber
 Structure and type of optical cable
 Discussion on measurement method of characteristic impedance of RF coaxial cable
 What is a fiber optical feeder cable
 Zhejiang Linquick Technology will participate in the 134th Canton Fair
 Introduction to RF coaxial cable
 Five common cable classification
 What is FTTA Remote Cable
 Test for insulation and sheath thickness of wire and cable products
 Congratulations to Zhejiang Linquick 24th CIOE a complete success
 Structure and type of optical cable
 Outdoor optical cables: the link that connects the world
 Wire and cable quality test three important indicators
 Laying method of communication optical cable
 Teach you to identify and choose coaxial cable and twisted pair
 Overview of material and structure of waterproof cable
 Process requirements and instructions for armored cables
 A brief discussion on the application of cluster wire
 Safety requirements and storage methods for wire and cable use
 Zhejiang Linquick NETCOM2023 exhibition was successfully held